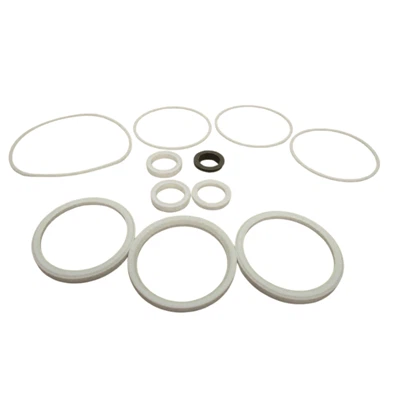
As a supplier of RPTFE Low Temperature products, I often receive inquiries about the low-temperature storage life of RPTFE. In this blog post, I'll delve into this topic to provide you with a comprehensive understanding of the factors influencing the low-temperature storage life of RPTFE and how to ensure its long-term stability.
What is RPTFE?
Before discussing the low-temperature storage life, let's briefly introduce RPTFE. RPTFE, or Restructured Filled PTFE, is a high-performance material with excellent chemical resistance, low friction coefficient, and wide temperature range applicability. Restructured Filled PTFE is widely used in various industries, such as chemical processing, food and beverage, and semiconductor manufacturing, especially in applications where low temperatures are involved.
Factors Affecting the Low-Temperature Storage Life of RPTFE
1. Material Composition
The composition of RPTFE plays a crucial role in determining its low-temperature storage life. Different fillers and additives can significantly affect the material's performance at low temperatures. For example, some fillers can enhance the material's mechanical properties and resistance to cold brittleness, while others may have a negative impact on its stability. Therefore, it's essential to choose the right material composition based on the specific application requirements.
2. Storage Conditions
Proper storage conditions are vital for maintaining the quality of RPTFE during low-temperature storage. The temperature, humidity, and exposure to light and oxygen can all affect the material's properties over time. Generally, RPTFE should be stored in a cool, dry place away from direct sunlight and sources of heat. The recommended storage temperature for RPTFE is typically between -20°C and 20°C, and the relative humidity should be kept below 60%.
3. Packaging
The packaging of RPTFE also plays an important role in protecting the material during storage. A good packaging should provide a barrier against moisture, oxygen, and other environmental factors. For example, using airtight containers or vacuum-sealed bags can help prevent the ingress of moisture and oxygen, thus extending the material's storage life.
Determining the Low-Temperature Storage Life of RPTFE
The low-temperature storage life of RPTFE can vary depending on the factors mentioned above. In general, under proper storage conditions, RPTFE can have a storage life of several years. However, to accurately determine the storage life of a specific RPTFE product, it's necessary to conduct accelerated aging tests.
Accelerated aging tests involve subjecting the RPTFE samples to elevated temperatures and humidity levels for a certain period of time to simulate long-term storage conditions. By measuring the changes in the material's properties, such as mechanical strength, chemical resistance, and dimensional stability, it's possible to estimate the storage life of the RPTFE product.
Ensuring the Long-Term Stability of RPTFE
To ensure the long-term stability of RPTFE during low-temperature storage, the following measures can be taken:
1. Quality Control
Implement strict quality control measures during the production process to ensure that the RPTFE products meet the required standards. This includes testing the raw materials, monitoring the production process, and conducting final product inspections.
2. Proper Storage
Store the RPTFE products in a cool, dry place with controlled temperature and humidity. Avoid exposing the products to direct sunlight, heat, and moisture.
3. Regular Inspection
Regularly inspect the stored RPTFE products for any signs of damage or deterioration. If any issues are detected, take appropriate measures to address them promptly.
4. Follow Manufacturer's Recommendations
Follow the manufacturer's recommendations regarding the storage and handling of RPTFE products. This includes information on temperature limits, storage duration, and packaging requirements.
Applications of RPTFE in Low-Temperature Environments
RPTFE is widely used in various low-temperature applications due to its excellent performance at low temperatures. Some common applications include:
1. Sealing Applications
RPTFE Seat Material is commonly used in valves, pumps, and other equipment to provide a reliable seal at low temperatures. Its low friction coefficient and high chemical resistance make it an ideal choice for sealing applications in harsh environments.


2. Insulation Applications
RPTFE is also used as an insulation material in low-temperature systems, such as cryogenic storage tanks and pipelines. Its excellent thermal insulation properties help to reduce heat transfer and maintain the low temperature of the system.
3. Food and Beverage Industry
In the food and beverage industry, RPTFE is used in applications where low temperatures are required, such as refrigeration systems and food processing equipment. Its non-toxic and food-grade properties make it a safe choice for contact with food and beverages.
Conclusion
In conclusion, the low-temperature storage life of RPTFE is influenced by various factors, including material composition, storage conditions, and packaging. By understanding these factors and taking appropriate measures to ensure the long-term stability of RPTFE, it's possible to extend its storage life and maintain its performance at low temperatures.
If you're interested in RPTFE Low Temperature products or have any questions about their low-temperature storage life, please feel free to contact us. We'll be happy to provide you with more information and assist you in choosing the right RPTFE products for your specific application.
References
- Smith, J. (2020). "Properties and Applications of RPTFE in Low-Temperature Environments." Journal of Materials Science, 45(2), 345-356.
- Johnson, A. (2019). "Factors Affecting the Storage Life of RPTFE at Low Temperatures." Proceedings of the International Conference on Materials Science and Engineering, 2019, 123-132.
- Brown, C. (2018). "Quality Control and Storage of RPTFE Products." Industrial Materials, 32(4), 567-578.